Puffy Air Pre-Cooler


Overview Yipu Associated Gas Pre-Cooler delivers four core values through professional technologies: This product is an ideal solution for resource utilization, energy conservation, and emission reduction of oilfield associated gas, particularly suitable for various associated gas recovery and utilization scenarios. I. Market Pain Point Analysis II. System Process Flow Six-Stage Intelligent Processing System: III. Working…
Overview
Yipu Associated Gas Pre-Cooler delivers four core values through professional technologies:
- Significant Economic Benefits: Pressure energy recovery reduces energy consumption by 40%; light hydrocarbon recovery rate increases by 25% to boost revenue; investment payback period of 1-1.5 years.
- Outstanding Environmental Benefits: Reduces associated gas venting and flaring; lowers greenhouse gas emissions; complies with environmental policy requirements.
- Stable and Reliable Operation: Ultra-wide operating condition adaptability; intelligent anti-fluctuation control; guaranteed long-term stable operation.
- Convenient Intelligent Operation & Maintenance: Remote monitoring and O&M; predictive maintenance; reduces O&M costs.
This product is an ideal solution for resource utilization, energy conservation, and emission reduction of oilfield associated gas, particularly suitable for various associated gas recovery and utilization scenarios.
I. Market Pain Point Analysis
- Complex and Volatile Compositions
- Associated gas methane content ranges from 30% to 70%, with high levels of heavy hydrocarbons such as ethane and propane.
- Contains impurities including crude oil droplets, formation water, and hydrogen sulfide (H₂S).
- Traditional equipment struggles to adapt to drastic composition changes.
- Unstable Pressure and Temperature
- Wellhead pressure rapidly depletes from 8.0MPa to atmospheric pressure.
- Temperature varies significantly with seasons and production stages (20-80℃).
- Conventional pre-cooling equipment operates inefficiently over a wide range of working conditions.
- Severe Energy Waste
- Large volumes of associated gas are directly vented and flared, resulting in resource waste.
- Pressure energy is not effectively recovered and utilized.
- Traditional equipment has high energy consumption, leading to significant operating cost pressure.
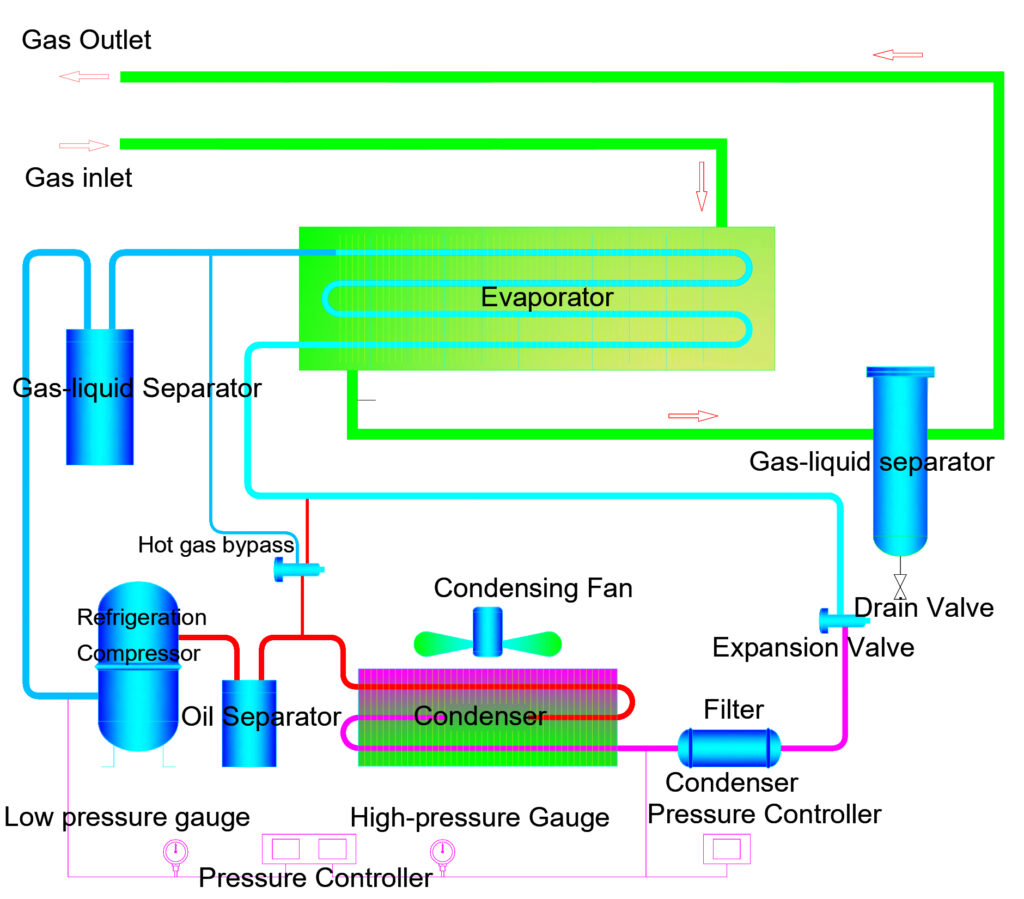
II. System Process Flow
Six-Stage Intelligent Processing System:
- Wellhead Pressure Energy Recovery
- High-pressure associated gas (≤8.0MPa) enters the expander power generation unit.
- Pressure energy is recovered, and the gas is pre-cooled to an intermediate temperature.
- Crude Oil Droplet Separation
- Expanded gas enters the high-efficiency cyclone separator.
- Carried crude oil droplets and solid particles are separated.
- Deep Pre-Cooling Treatment
- Gas enters the plate-fin main heat exchanger.
- Deep heat exchange with the refrigerant enables precise temperature control.
- Heavy Hydrocarbon Condensation and Separation
- Pre-cooled gas enters the three-phase separator.
- Effective separation of light hydrocarbons, water, and dry gas is achieved.
- Product Gas Precision Treatment
- Separated dry gas enters the precision filter.
- Ensures product gas quality meets standards.
- Intelligent Monitoring and Regulation
- PLC automatically optimizes operating parameters based on real-time working conditions.
- Ensures the system operates at the optimal working point.
III. Working Principle
Multiphase Flow Deep Heat Exchange Technology:
- Specially designed anti-clogging heat exchanger flow channels.
- Adapts to the complex flow of oil-gas-water mixtures in associated gas.
- Anti-scaling and anti-clogging design ensures long-term stable operation.
Intelligent Anti-Fluctuation Control:
- Adaptive control algorithm based on pressure depletion curves.
- Multivariable coordinated control to cope with drastic composition changes.
- Three-level safety interlock protection system.
IV. Core Advantages
- Ultra-Wide Operating Condition Adaptability
- Operating pressure range: 0.05-8.0MPa.
- Adapts to associated gas with methane content of 30%-70%.
- Stable processing effect during pressure and temperature fluctuations.
- Efficient Energy Recovery System
- Integrates pressure energy power generation, reducing energy consumption by 40%.
- Intelligent thermal management maximizes energy utilization efficiency.
- Light hydrocarbon recovery rate increased by over 25%.
- Strong Anti-Pollution Capability
- Special materials resist hydrogen sulfide corrosion.
- Anti-scaling design extends equipment service life.
- Intelligent cleaning system reduces maintenance frequency.
- Rapid Deployment and Intelligent O&M
- Integrated skid-mounted design shortens on-site installation cycle by 70%.
- Remote intelligent monitoring reduces O&M costs by 30%.
V. Technical Strength
Core Technology Patents:
- Associated gas multiphase flow deep heat exchange technology.
- High-efficiency cascade utilization technology of pressure energy.
- Intelligent anti-fluctuation control algorithm.
- Online anti-clogging early warning system.
Manufacturing Process Advantages:
- Application of special materials for acid-resistant environments.
- Professional manufacturing qualification for high-pressure systems.
- Strict on-site testing and verification.
VI. Product Series Introduction
Specialized Series Configuration:
- YP-AGP-150 Series: 60-500 Nm³/min (Single Well/Well Group)
- YP-AGP-500 Series: 600-2000 Nm³/min (Small Gas Gathering Station)
- YP-AGP-2000 Series: 2500-5000 Nm³/min (Medium-Sized Processing Station)
- YP-AGP-5000 Series: 6000-10000 Nm³/min (Large-Scale Processing Center)
Special Configuration Options:
- Special version for high-sulfur working conditions.
- Thermal insulation version for extremely cold regions.
- Explosion-proof version for offshore platforms.
- Intelligent remote O&M system.
VII. Application Scenarios
Oilfield Extraction Scenarios:
- Associated gas recovery and utilization at single wells, centralized processing of cluster well groups, associated gas recovery from marginal oilfields.
Gathering and Processing Scenarios:
- Front-end pre-cooling at gathering stations, pre-treatment for light hydrocarbon recovery units, pre-treatment of feed gas for natural gas processing plants.
Energy Utilization Scenarios:
- Feed gas processing for gas-fired power generation, gas source processing for oilfield gas injection systems, gas source processing for fuel gas systems.
Environmental Protection Scenarios:
- Vent gas recovery processing, flare gas recovery and utilization, pre-treatment for VOC control.
VIII. Detailed Technical Specifications
| Parameter Category | Technical Indicators | Remarks |
|---|---|---|
| Operating Conditions | ||
| Inlet Air Temperature | 20-80℃ | Adapts to wellhead temperature changes |
| Working Pressure | 0.05-8.0 MPa | Standard: 0.7 MPa, ultra-wide pressure range |
| Gas Composition | Customized on demand | Adapts to characteristics of different oilfield associated gases |
| Performance Indicators | ||
| Pressure Dew Point | ≤2℃~15℃ | Precisely controlled to meet pipeline transportation requirements |
| Pressure Loss | ≤0.05 MPa | Low-resistance energy-saving design |
| Gas Processing Capacity | 60-10000 Nm³/min | Full series coverage |
| Light Hydrocarbon Recovery Rate | ≥95% | Efficient recovery of C3+ components |
| Technical Configuration | ||
| Working Cycle | Continuous operation | Adapts to continuous oilfield production requirements |
| Control Mode | PLC programmable control | Fully automatic intelligent operation |
| Installation Method | Indoor flat ground, no foundation required | Rapid deployment |
| Utility Requirements | ||
| Cooling Water Pressure | 0.2~0.4 MPa | Industrial circulating water |
| Cooling Water Temperature | ≤32℃ | |
| Power Supply | 380V/50HZ | |
| Structural Parameters | ||
| Equipment Weight | 4100~18500 kg | Heavy-duty equipment, stable and reliable |
| Overall Dimensions (L×W×H) | L(1050~8000)×W(2100~3300)×H(2200~3000) mm | Integrated skid-mounted design |
| Explosion-Proof Grade | Exd II BT4 | Higher grades available as an option |