VPSA Pressure Swing Adsorption Oxygen Generator


Yipu VPSA (Vacuum Pressure Swing Adsorption) Oxygen Generator has successfully addressed the economic challenges of medium-scale oxygen demand scenarios through innovations in vacuum adsorption technology. Its core value lies in: providing one of the optimal technical paths for oxygen demand of 50-6000 Nm³/h, reducing the comprehensive operating cost by 35-50% compared with traditional solutions, significantly…
Yipu VPSA (Vacuum Pressure Swing Adsorption) Oxygen Generator has successfully addressed the economic challenges of medium-scale oxygen demand scenarios through innovations in vacuum adsorption technology. Its core value lies in: providing one of the optimal technical paths for oxygen demand of 50-6000 Nm³/h, reducing the comprehensive operating cost by 35-50% compared with traditional solutions, significantly lowering labor costs through an intelligent operation and maintenance system, and perfectly matching various application scenarios with a modular design. This equipment is particularly suitable for metallurgical enterprises undergoing energy-saving transformation, new sewage treatment projects, and distributed energy stations, and is one of the core equipment for achieving low-carbon production.
I. Market Pain Point Analysis
High Cost of Traditional Oxygen Supply Modes
- Transportation and storage costs of liquid oxygen storage tanks and bottled oxygen account for more than the value of oxygen itself.
- Cryogenic air separation equipment requires high investment intensity (investment per cubic meter of oxygen exceeds 3,000 yuan), suitable for large-scale centralized oxygen supply.
Prominent Energy Efficiency Bottlenecks
- The power consumption of traditional PSA oxygen generation is as high as 0.45-0.55 kWh/Nm³.
- Cryogenic oxygen generation has a long startup time (8-12 hours) and cannot adapt to load fluctuations.
Difficulties in Matching Medium-Scale Demand
- There is a supply gap for medium-scale demand of 5-6000 Nm³/h.
- Existing equipment lacks economical solutions in the purity range of 70%-94%.
High Requirements for Operation and Maintenance Support
- Traditional equipment has low automation and requires professional technical personnel on duty.
- Molecular sieves have a short service life (usually 2-3 years) and high replacement costs.
II. System Process Flow
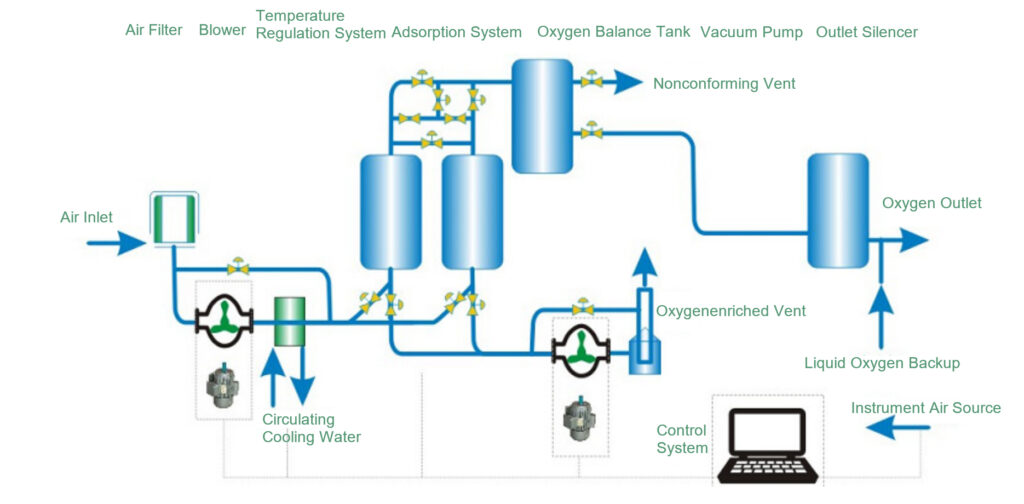
Core System Configuration
- Power System: Roots blower + roots vacuum pump unit
- Separation System: Dual-tower/multi-tower adsorber (filled with lithium-based molecular sieves)
- Control System: PLC + pneumatic switching valve group
- Gas Storage System: Oxygen balance tank + pressure buffer device
Five-Step Cycle Process
- Pressurized Adsorption Stage
- Roots blower pressurizes filtered air to 25-35 kPa.
- Air enters the adsorber, and molecular sieves preferentially adsorb nitrogen (kinetic diameter 3.64 Å).
- The purity of the produced oxygen gradually increases to the set value.
- Pressure Equalization and Depressurization Stage
- The oxygen-rich gas (0.2-0.3 MPa) in the adsorber is introduced into the regeneration tower.
- Recovers more than 85% of pressure energy and reduces system energy consumption.
- Vacuum Desorption Stage
- Roots vacuum pump evacuates the tower pressure to -65~-75 kPa.
- The adsorbed nitrogen, CO₂, and water molecules are completely desorbed.
- Pressure Equalization and Pressurization Stage
- Uses oxygen-rich gas from other towers for pre-pressurization to reduce blower energy consumption.
- Product Gas Pressurization Stage
- Oxygen booster increases the product gas pressure to 0.4-0.8 MPa.
- Enters the balance tank to stabilize pressure fluctuations.
III. In-Depth Analysis of Technical Principles
Molecular Sieve Adsorption Mechanism
- Adopts LiX-type lithium-based molecular sieves with an N₂/O₂ separation coefficient of 4.5-5.2.
- Based on the strong interaction between the nitrogen quadrupole moment effect (1.3×10⁻²⁶ esu·cm²) and molecular sieve cations.
- Oxygen molecules (without dipole moment) are basically not adsorbed, achieving efficient separation.
Vacuum-Enhanced Regeneration
- The relationship between vacuum degree and nitrogen desorption capacity is exponential (desorption rate reaches 92% at -65 kPa).
- Saves 25-35% more energy than traditional PSA and improves molecular sieve utilization by 40%.
IV. Core Competitive Advantages
Industry-Leading Energy Consumption Indicators
- Unit power consumption: 0.32-0.38 kWh/Nm³ (at 93% purity).
- Saves 30% more electricity than traditional PSA and 50% more than cryogenic method.
Intelligent Control System
- Equipped with adaptive optimization algorithm to automatically track load changes.
- Closed-loop purity control with fluctuation range < ±0.5%.
Long-Service-Life Design
- Molecular sieve wear resistance > 98% with service life ≥ 8 years.
- Valve cycle life > 3 million times with annual failure rate < 0.5%.
Modular Architecture
- Standard modules: 50/100/200 Nm³/h, parallel connection up to 6000 Nm³/h.
- Installation cycle is 60% shorter than traditional equipment.
V. Reflection of Technical Strength
Application of Innovative Technologies
- Isothermal adsorption model predictive control technology.
- Four-tower rapid switching process (cycle 90-120 seconds).
- Heat-coupled vacuum cooling system.
Performance Guarantee System
- Molecular sieve packing density control accuracy ±1.5%.
- Gas flow distribution uniformity deviation < 5%.
- Online purity analyzer accuracy: Class 0.1.
VI. Product Series Introduction
Standard Model Configuration
- VPSA-50 Series: 50-500 Nm³/h (basic industrial use)
- VPSA-100 Series: 500-2000 Nm³/h (metallurgy, chemical industry)
- VPSA-200 Series: 2000-6000 Nm³/h (large-scale projects)
Special Customized Models
- Explosion-proof type (Ex d Ⅱ CT4)
- High-altitude type (effective at 3000 meters above sea level)
- Container type (all-weather protection class IP55)
VII. Application Scenario Solutions
Customized Solutions for Metallurgical Industry
- Electric furnace steelmaking: 93% purity, 0.8 MPa pressure.
- Blast furnace oxygen enrichment: 70-80% purity, large-flow continuous oxygen supply.
Applications in Environmental Protection Field
- Sewage treatment: Oxygen utilization rate increased to 35-40%.
- Waste incineration: Combustion-supporting oxygen reduced by 20%, flue gas emissions reduced by 30%.
Medical and Health Configuration
- Medical oxygen standard (GB 8982-2009)
- Dual-unit redundant backup with online switching < 3 seconds.
VIII. Detailed Technical Indicators
Performance Parameters
| Parameter Item | Technical Indicators / Description |
|---|---|
| Output Range | 5-6000 Nm³/h (supports modular expansion) |
| Oxygen Purity | 70%-94% (adjustable online) |
| Outlet Pressure | VPSA direct output ≤ 20 kPa; after pressurization ≤ 0.8 MPa |
| Dew Point Temperature | ≤ -60℃ (atmospheric pressure) |
Energy Efficiency Indicators
| Parameter Item | Technical Indicators / Description |
|---|---|
| Specific Power Consumption | 0.32-0.45 kWh/Nm³ (varies with purity) |
| Cooling Water Consumption | ≤ 0.5 m³/h (water-cooled type only) |
| Noise Level | ≤ 82 dB(A) |
Reliability Indicators
| Parameter Item | Technical Indicators / Description |
|---|---|
| Continuous Operation Time | ≥ 8000 hours |
| Automatic Control Rate | 100% |
| Load Regulation Range | 30-110% |